
Custom Machine Tool Bed & Base Castings
Kurt Foundry casts grey iron beds, bases, columns and tables for machine builders, poured to your drawing in single castings up to 1,000 kg and CNC machined in-house.
A Stable Foundation Starts in the Foundry
A machine is only as accurate as the casting it is built on. Porosity under a slideway, a rib that cools unevenly, or residual stress that relaxes after machining will show up later as chatter, drift and lost tolerance. Kurt Foundry casts machine tool beds and bases in grey iron, where the graphite structure damps vibration and machines cleanly, and controls chemistry, cooling and finishing so the part stays true after it leaves our shop.
We work from your 2D drawing or 3D model, review rib layout and wall sections with your engineers, and deliver castings rough-machined or finish-machined, ready for assembly.
What We Customize for You
Every bed and base is cast to your design, not pulled off a shelf. These are the details we engineer with you before the pattern is made.
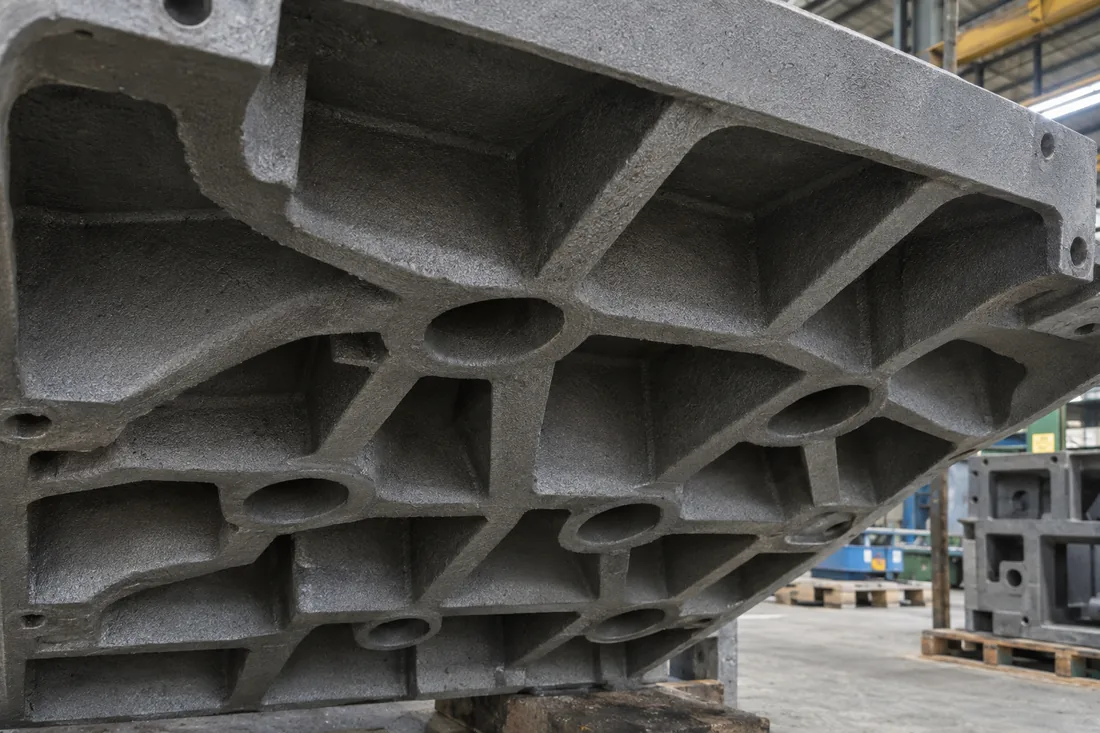
Rib Layout & Wall Sections
Box sections, cross ribs and lightening holes are laid out for stiffness per kilogram, with wall transitions reviewed for even cooling so heavy guideway sections stay dense.
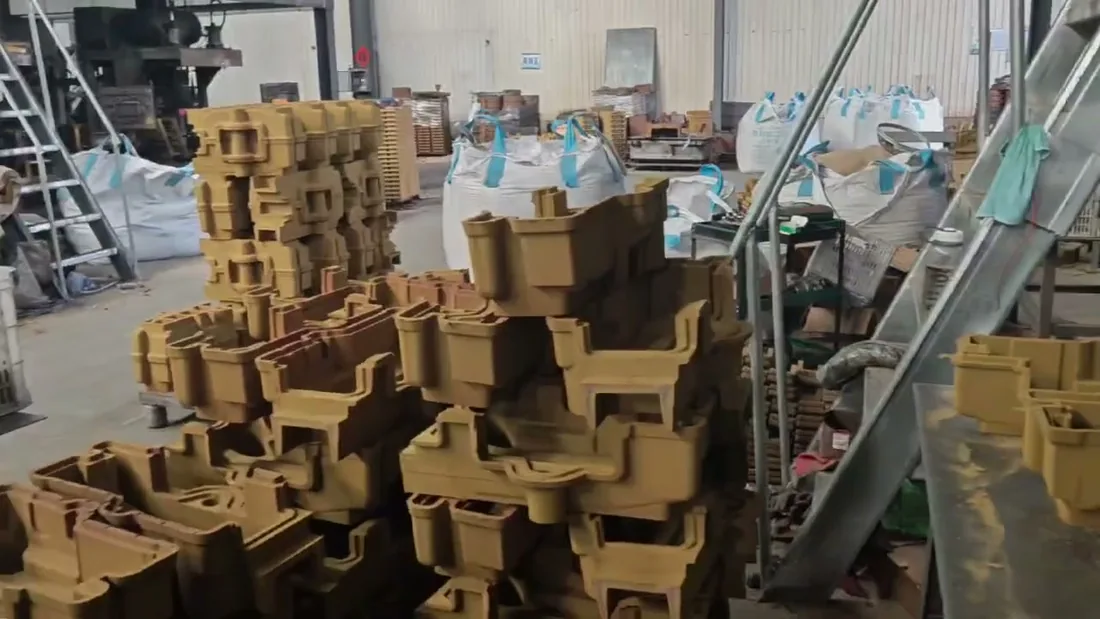
Cores & Internal Cavities
Sand cores form the hollow sections, coolant channels, chip troughs and cable paths inside the casting, cutting weight while keeping the walls you need for rigidity.
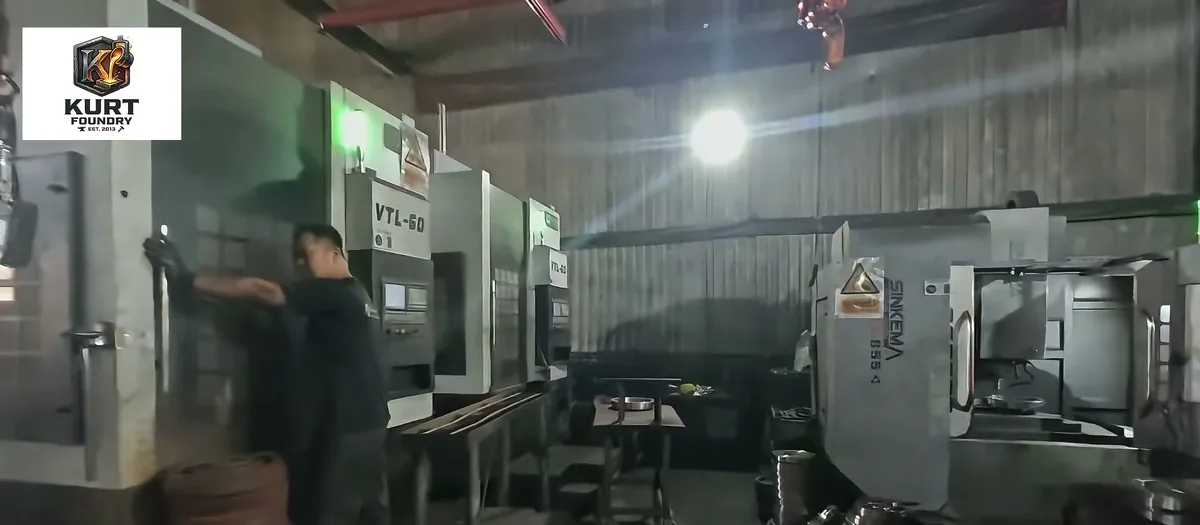
Guideway & Mounting-Face Machining
Slideways, mounting pads, datum faces and bolt patterns are machined in-house to your drawing, so the casting arrives ready for rails, spindles and leveling feet.
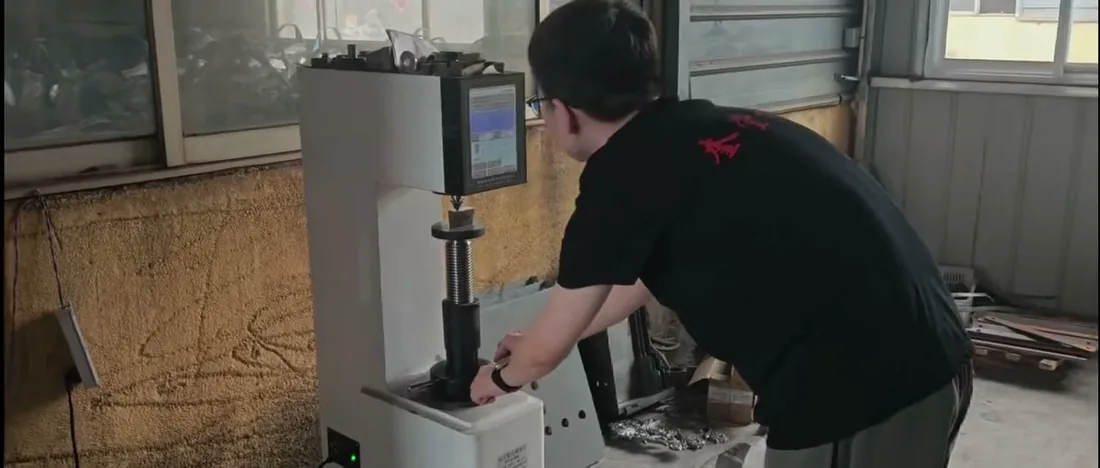
Grade & Hardness Verification
Chemistry and hardness are checked against the grade on your drawing, so wear surfaces and bolt bosses perform the same on every casting in the batch.
Material Grades for Machine Tool Castings
Not sure which grade fits? Compare all custom iron castings options or try our material grade advisor.
Grey iron is the standard choice for beds and bases. Ductile iron is used where a part also has to take shock or bending loads.
| Standard / Grade | Nearest Equivalents | Min. Tensile Strength (MPa) | Typical Machine Tool Use |
|---|---|---|---|
| ASTM A48 Class 30 (Grey Iron) | HT200 / EN-GJL-200 | 207 | Light-duty bases, covers, stands and guards. |
| ASTM A48 Class 35 (Grey Iron) | HT250 / EN-GJL-250 | 241 | Lathe beds, machining-center bases and columns; the most common choice. |
| ASTM A48 Class 40 (Grey Iron) | HT300 / EN-GJL-300 | 276 | Heavier-loaded beds, columns and saddles with wide slideways. |
| ASTM A536 65-45-12 (Ductile Iron) | QT450-10 / EN-GJS-450-10 | 448 | Tables, brackets and arms that also see shock or bending loads. |
Where These Castings Are Put to Work
Typical machine tool and equipment castings we quote, sized for single castings from 1 kg up to 1,000 kg (2,200 lbs).
Lathe Beds & Headstocks
Beds with integral slideways, headstock and tailstock housings for bench, toolroom and small CNC lathes.
Machining-Center Bases & Columns
Bases, columns, saddles and tables for compact vertical machining centers, drilling and tapping machines.
Grinder, Press & Test-Rig Bases
Rigid, vibration-damping bases for surface grinders, small presses, inspection stands and test equipment.
How We Manufacture Your Machine Tool Castings
From pattern to machined datum faces, every step is aimed at one thing: a casting that stays dimensionally stable after machining.
1. Pattern & DFM Review
We review your model for rib layout, wall-thickness transitions, core supports and riser placement on heavy guideway sections, then build the pattern and core boxes.
2. Molding & Core Setting
Sand cores for the internal cavities are made and set into the mold, and core positions are checked before the mold is closed.
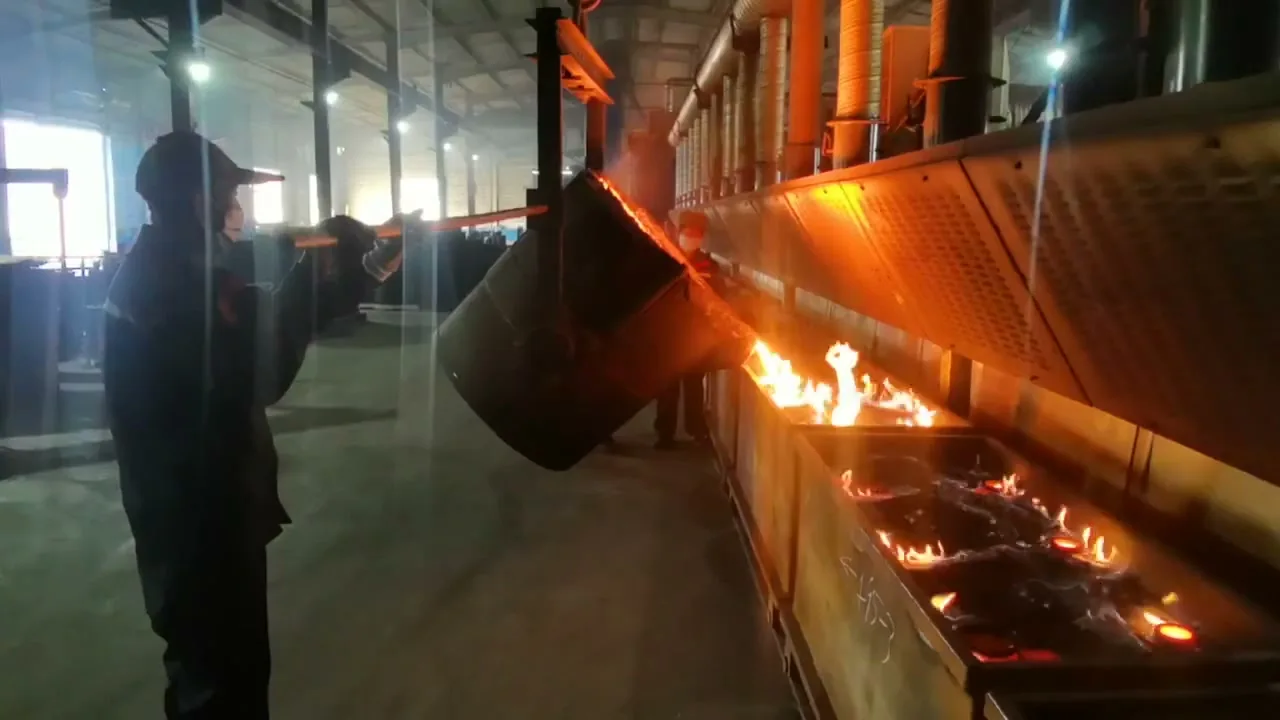
3. Spectrometer-Verified Melting & Pouring
Each melt is checked by spectrometer before pouring, so carbon equivalent and alloy content match the grade on your drawing.
4. Controlled Cooling & Shakeout
Castings cool in the mold before shakeout to limit thermal stress between thick slideway sections and thinner ribs.
5. Stress Relief Before Machining
Beds and bases are stress-relieved by thermal aging before machining, so the casting does not move once the slideways are cut.
6. Shot Blasting & Fettling
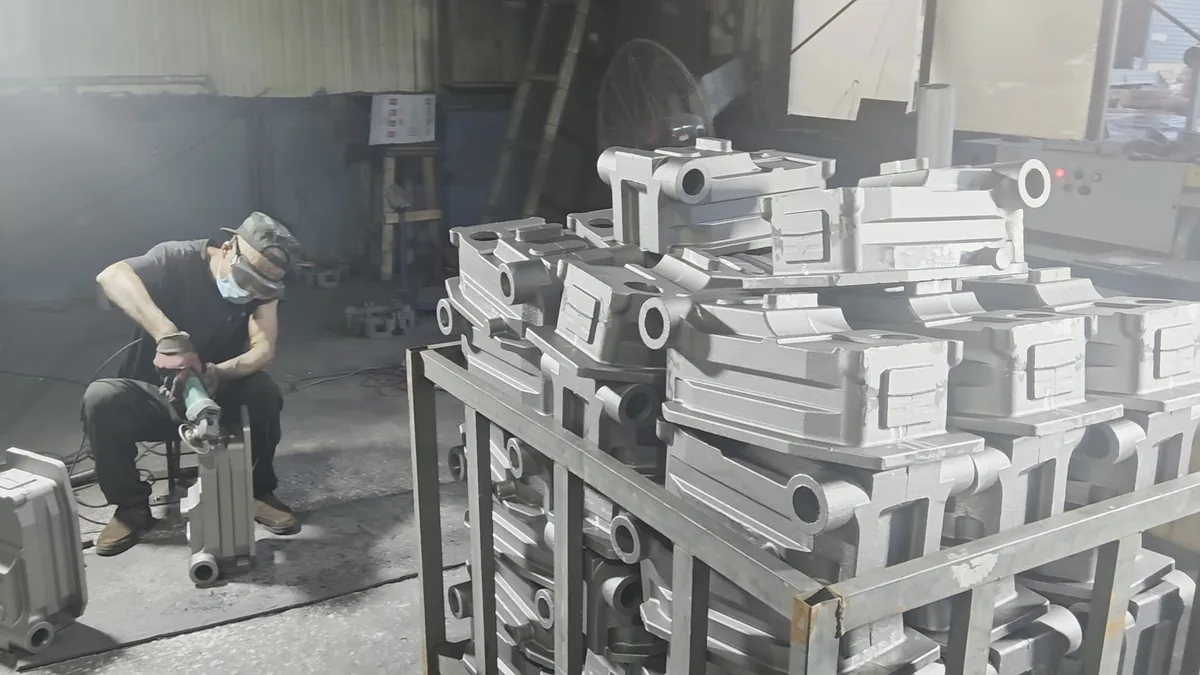
Sand is shot-blasted off, and gates, risers and parting lines are ground flush, ready for primer or machining.
7. CNC Machining & Final Inspection
Datum faces, slideways, pads and holes are machined in-house, then checked against your drawing before painting and packing.
Quality Control for Machine Tool Castings
Every bed and base is checked for chemistry, hardness and geometry before it leaves the foundry, under our IATF 16949:2016 quality system.
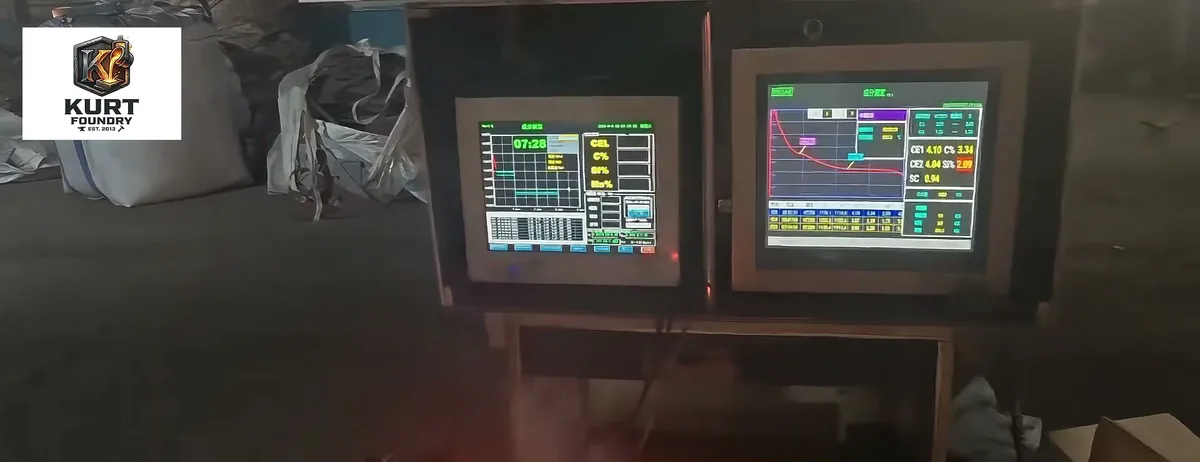
- Chemical Analysis:Spectrometer results for every melt are recorded and supplied as Material Test Reports (MTRs) with your shipment.
- Hardness Testing:Brinell hardness is checked on the casting to confirm the grade and the consistency of wear surfaces.
- Mechanical Testing:Tensile test bars poured with the casting verify the grade’s minimum strength when your specification requires it.
- Dimensional & Surface Inspection:Machined faces, hole patterns and slideways are measured against your drawing, and machined surfaces are inspected for sand inclusions and porosity.
Worldwide Export Shipping — Direct from Foundry
Kurt Foundry exports to customers across North America, Europe, Southeast Asia, the Middle East and Australia, and manages logistics from our foundry floor to your receiving dock.
We ship FOB, CIF or DDP from Qingdao, with one direct-factory price and full freight transparency.
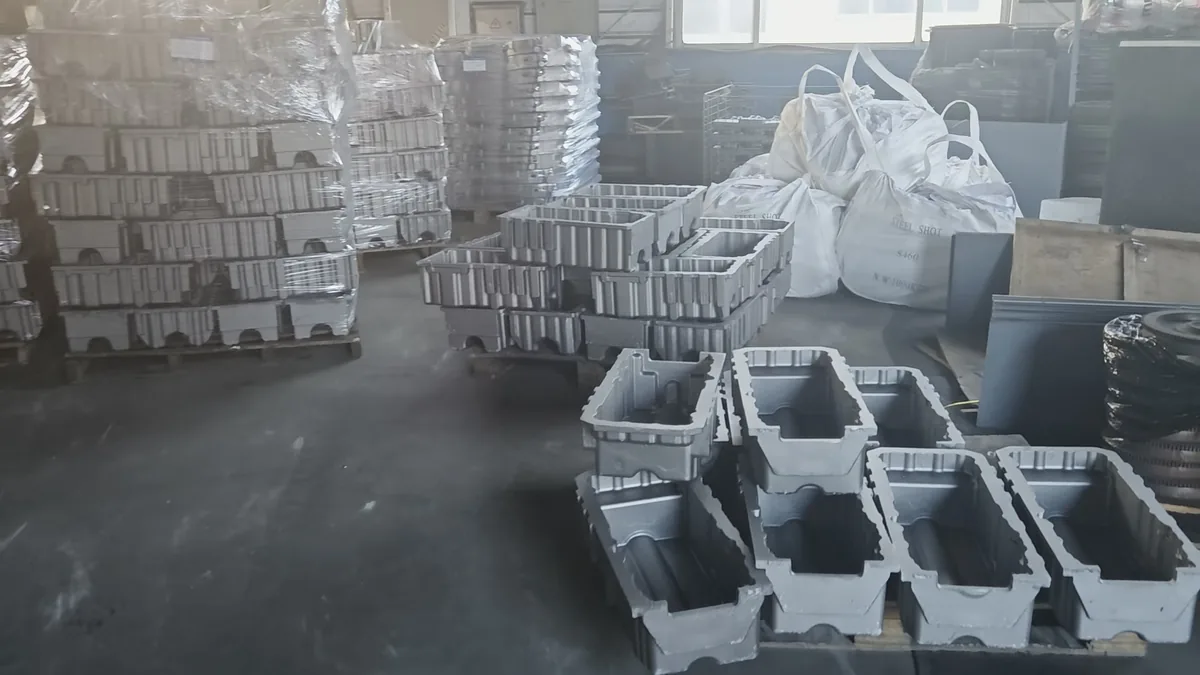
Machined faces are rust-protected, and beds and bases are secured on skids or in ISPM-15 fumigated wooden crates so slideways are not damaged in transit.
Ocean Freight
Full-container or LCL ocean freight from Qingdao to ports in the USA, Canada, Europe, Southeast Asia, the Middle East and Australia.
Flexible Trade Terms
FOB, CIF and DDP terms to fit your procurement process and import requirements.
Last-Mile Delivery
Under DDP we handle customs clearance and inland trucking to your facility in the USA, Canada and selected European destinations.
Export Packing
Rust-preventive coating on machined faces, skids or fumigated crates, and full export documentation.
Why Choose Kurt Foundry for Machine Tool Castings
Cast, finished and machined under one roof, with one team responsible from pattern to packed part.
Grey Iron Specialists
Grey and ductile iron are our core work, the same metallurgy we use on engine flywheels under our IATF 16949:2016 certification.
Casting and Machining in One Place
No hand-off between a foundry and a machine shop: the team that pours your bed also machines its datum faces.
Prototype to Production
Orders start at one piece for a prototype machine, and the same pattern carries through to production batches.
Related Castings
Other machined iron housings we cast for equipment builders.
Gearbox Housings
Grey and ductile iron gearbox and reducer housings, bored and faced in-house.
Bearing Housings
Pillow blocks and bearing housings machined to your bore and bolt pattern.
Grey Iron Castings
Our full grey iron capability, grades and testing.
Frequently Asked Questions
We pour single castings from 1 kg up to 1,000 kg (2,200 lbs), which covers beds, bases and columns for small and mid-size machines. For a heavier design, our engineers can review splitting the bed into bolted sections.
The graphite flakes in grey iron damp vibration far better than steel, it machines cleanly, holds its shape well once stress-relieved, and wears well on slideways. That is why ASTM A48 Class 35 (HT250) is the usual choice for beds and bases.
Yes. Beds and bases are stress-relieved by thermal aging before machining, so the casting does not move after the slideways and datum faces are cut.
Yes. We machine datum faces, slideways, mounting pads and bolt holes in-house to your drawing. Send your tolerances and we will confirm what we hold in-house and quote any final grinding or scraping separately.
Orders start at one piece for prototypes. We return DFM feedback and a quote within 48 hours; tooling takes 3 to 4 weeks, and production follows 4 to 6 weeks after sample approval.
Ready to Quote Your Machine Tool Castings?
Send your drawing or 3D model, and we’ll return DFM feedback and a quote within 48 hours.
Get a Free Quote